| Impulse heat sealer |
An electric element heats briefly when the operator presses the sealing arm. Pressure holds the material together as it cools and forms a seal. |
Many heat-sealable thermoplastics, including polyethylene and some laminated films. Compatibility depends on the film structure and thickness. |
Intermittent sealing of small or medium quantities, such as packaging parts, samples, and general goods. |
Heats only during the sealing cycle, so it generally does not need a long warm-up. Available in manual and foot-operated formats. |
Seal time and pressure must be adjusted to the material. It is intended for intermittent use rather than uninterrupted high-volume production. |
| Constant-heat sealer |
Heated sealing bars remain at a set temperature and apply heat and pressure to the bag layers. |
Materials that require sustained heat, including some thicker films and heat-sealable laminates. |
Sealing heavier bags or materials that may not seal reliably with a brief impulse cycle. |
Provides continuous heat at the jaws and can suit materials needing a longer heat dwell. |
The sealing bars remain hot between cycles. Temperature and dwell time need careful control to reduce weak seals or film damage. |
| Continuous band sealer |
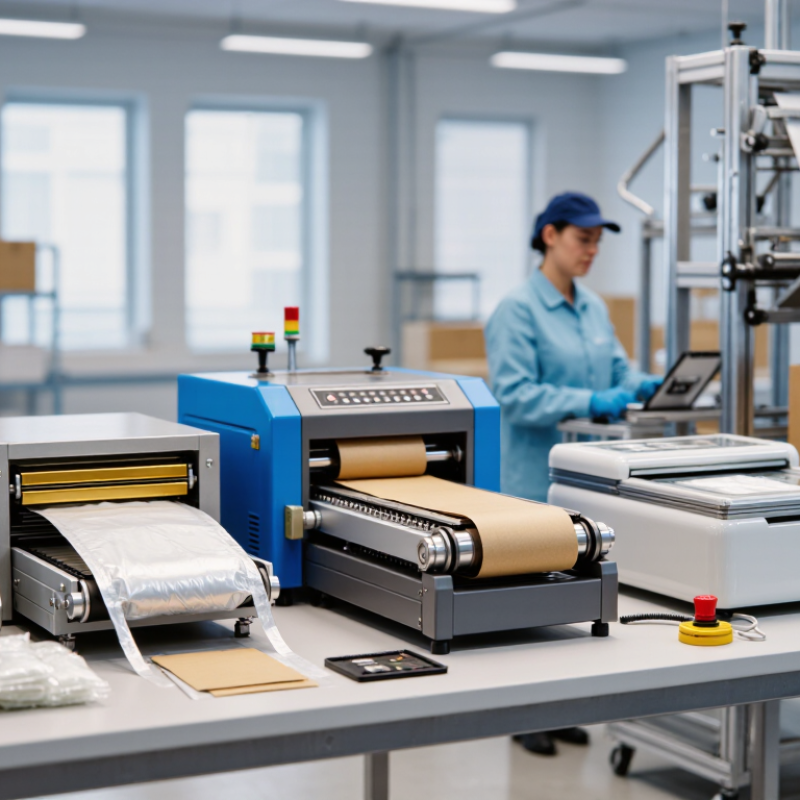
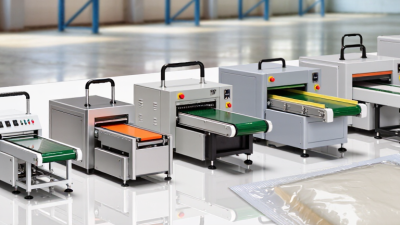
Conveyor belts carry bags between heated sealing blocks and pressure rollers, creating a seal as the bag moves through the machine. |
Compatible heat-sealable films and pouches; suitability varies with film construction and machine settings. |
Repeated sealing of many bags, including products packed on a production line. |
Supports a steady flow of bags and can seal longer runs without manually opening and closing a sealing jaw for every bag. |
Requires suitable bag presentation and consistent settings. Conveyor speed, temperature, and pressure affect seal quality. |
| Vacuum chamber sealer |
The open bag is placed inside a chamber. Air is removed, then a heated bar seals the bag before the chamber returns to normal pressure. |
Vacuum-compatible, heat-sealable bags, often multilayer barrier pouches. |
Packaging foods and other products when reduced air inside the package is required. |
Removes air from the chamber and bag before sealing; the chamber can also accommodate multiple bags in one cycle, depending on its size. |
Needs compatible bags and a suitable chamber. Vacuum packaging does not replace safe food handling or required storage conditions. |
| Nozzle vacuum sealer |
A nozzle draws air from the bag opening, after which sealing jaws close and heat-seal the film. |
Vacuum-compatible flexible bags designed for the machine and product. |
Vacuum packaging where a chamber-style machine is not practical, including some larger or irregularly shaped items. |
The nozzle can remove air directly from the bag without enclosing the whole package in a vacuum chamber. |
Bag opening placement and nozzle access matter. Product residue near the seal area can interfere with sealing. |
| Hot-bar or platen sealer |
One or two heated bars press the bag layers together for a controlled period to create a seal. |
Heat-sealable films and laminates that match the temperature, pressure, and dwell-time range of the equipment. |
Applications requiring a defined seal width or a controlled, repeatable sealing cycle. |
Can provide consistent pressure and dwell time, especially in semi-automatic or automated setups. |
Correct tooling and settings are essential. Not all plastics or coated materials are heat-sealable. |