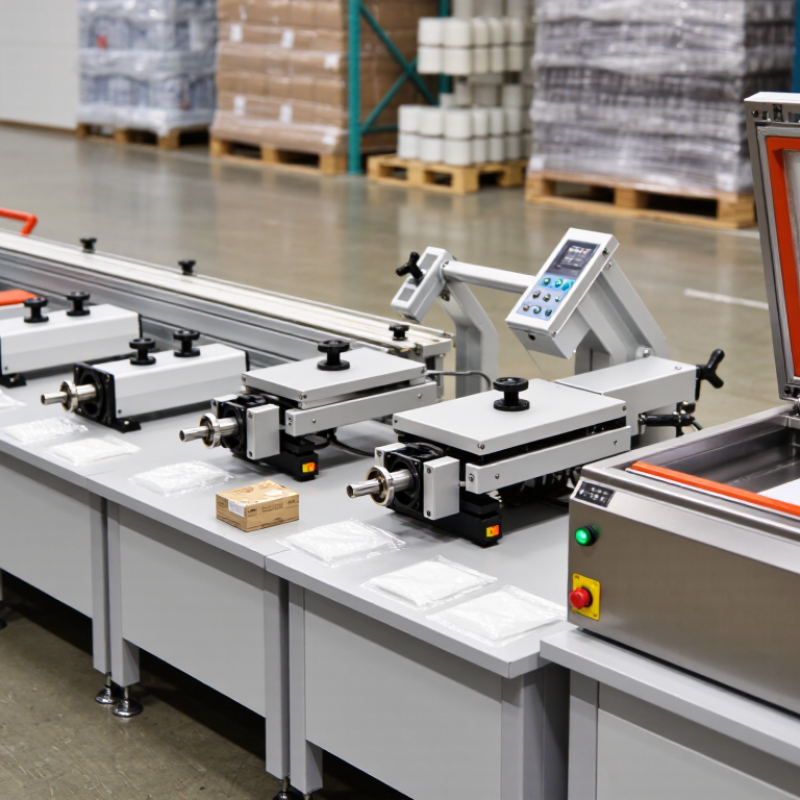
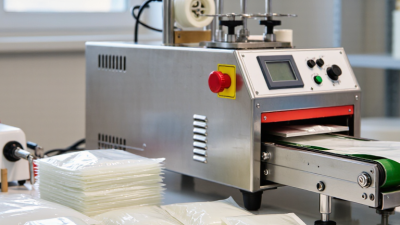
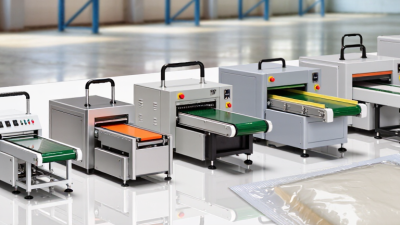
| Continuous Band Sealer |
Pre-made flat pouches and bags; horizontal product feeding |
PE, PP, laminated PET/PE, OPP/CPP, and foil-laminate bags |
Approximately 30–200 μm per layer or laminate, depending on construction |
Suited to repeatable production with consistent bag positioning. Check seal width, conveyor capacity, and compatibility with the pouch’s inner sealant layer. |
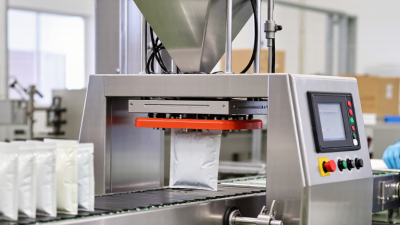
| Vertical Continuous Band Sealer |
Pre-made bags containing powders, granules, or liquids that should remain below the seal area |
PE, PP, PET/PE, and other heat-sealable laminated films |
Approximately 40–200 μm |
Vertical feeding helps keep product away from the seal zone. Confirm that the bag material, product dust, and fill level allow a clean, uninterrupted seal. |
| Constant-Temperature Hot-Bar Sealer |
Pre-made pouches, sachets, liners, and packages requiring a defined, wider seal |
PE and PP films; PET/PE, PA/PE, and foil-containing laminates with compatible sealant layers |
Approximately 50–300 μm |
Heated jaws apply controlled temperature, pressure, and dwell time. Useful for thicker materials, but settings must be validated for the specific laminate and seal width. |
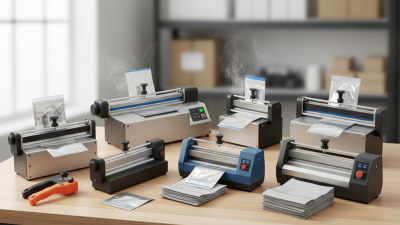
| Impulse Bar Sealer |
Intermittent sealing of bags, liners, and smaller production runs |
Commonly PE and PP films; some laminates designed for impulse sealing |
Approximately 40–250 μm |
The sealing element heats during the cycle and cools under pressure. Match the element length and control cycle to the film’s sealant layer and thickness. |
| Rotary Heat Sealer |
Continuous sealing of formed pouches, tubes, and selected flexible packages |
Heat-sealable PE or PP webs and compatible multilayer laminates |
Approximately 40–200 μm |
Rotating heated wheels support continuous operation. Check web tracking, seal geometry, and whether the package requires a longitudinal or transverse seal. |
| Vacuum Chamber Sealer |
Vacuum-packed bags for food, medical, or industrial products |
PA/PE vacuum pouches, PE-based bags, and suitable multilayer barrier pouches |
Approximately 60–200 μm |
Choose chamber size, pump capacity, and seal-bar configuration for the package dimensions and required vacuum level. The pouch must be designed for vacuum use. |
| Tray Sealer |
Rigid or semi-rigid trays with lidding film; modified-atmosphere or standard packs |
PP, PET, or CPET trays with compatible PE-, PP-, or PET-based lidding films |
Lidding film: approximately 30–100 μm; tray thickness varies by material and design |
Tray flange and lidding-film sealant must be compatible. Confirm tooling, peelability or weld strength, and any gas-flushing requirements. |
| Vertical Form-Fill-Seal (VFFS) Machine |
Pillow bags, gusseted bags, and related packs formed from a roll of film |
PE, PP, OPP/CPP, and laminated rollstock with a suitable heat-seal layer |
Approximately 30–120 μm |
Film stiffness, coefficient of friction, print registration, and sealant-layer orientation affect forming and sealing. Match the forming tube and jaw design to the bag style. |
| Horizontal Form-Fill-Seal (HFFS) / Flow Wrapper |
Wrapped solid products such as bars, bakery items, and multipacks |
OPP, CPP, PE, polyolefin films, and compatible printed laminates |
Approximately 20–80 μm |
Designed for products fed horizontally. Verify product dimensions, fin-seal configuration, end-seal pattern, and the film’s hot-tack performance at production speed. |
| L-Bar Shrink Sealer |
Single items or multipacks wrapped in shrink film, often followed by a heat-shrink tunnel |
Polyolefin shrink film and PVC shrink film where permitted and suitable |
Typically approximately 12–30 μm |
The L-shaped seal cuts and seals the film around the product. Film shrink behavior and package size determine seal settings and the need for a separate tunnel. |