| Thermal Printing Technology | Confirm whether the roll is for direct thermal printing or thermal-transfer printing. | Direct thermal labels use heat-sensitive coating and do not require a ribbon. Thermal-transfer labels require a compatible ribbon. | Product data sheet and a print sample tested on the intended printer. | The wrong label construction can cause poor image quality, printer issues, or unnecessary ribbon use. |
| Facestock and Coating | Specify paper or synthetic facestock, surface finish, and any top coating required for the application. | Common options include uncoated direct thermal paper, top-coated direct thermal paper, and synthetic facestock. | Technical data sheet stating material type and relevant performance properties. | Facestock selection affects print clarity and resistance to moisture, abrasion, oils, and handling. |
| Label Size and Layout | Give label width and height, gap or mark requirements, corner shape, and winding direction. | Dimensions should match the printer’s supported media width and sensor configuration; there is no single universal label size. | Dimensioned drawing or approved production sample. | Correct layout supports reliable feeding, sensing, and placement in the end-use application. |
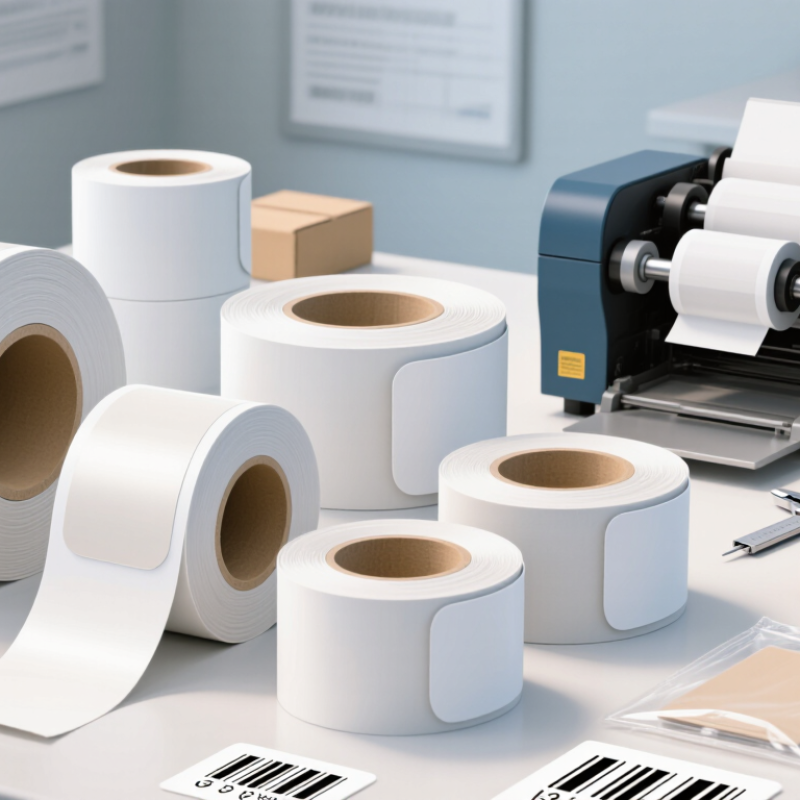
| Roll and Core Dimensions | State core inner diameter, maximum roll diameter, and labels per roll. | Core sizes and maximum roll diameters vary by printer and dispenser. Confirm both against the equipment manual. | Roll specification showing core diameter, outer diameter, and roll count. | Incompatible roll dimensions can prevent loading or reduce machine run time. |
| Adhesive Performance | Define the substrate, application temperature, service temperature, and whether removable or permanent adhesion is required. | Adhesive performance depends on the label material, surface energy, cleanliness, temperature, and contact time. | Adhesive technical data and test labels applied to the actual packaging or product surface. | A label that does not bond or remove as intended can create rework, returns, or product identification problems. |
| Print and Use Conditions | Describe exposure to heat, light, moisture, abrasion, chemicals, and expected storage duration. | Direct thermal image life varies with coating, print density, storage conditions, and exposure; request application-specific guidance. | Supplier test information and a sample evaluated under the intended conditions. | Direct thermal images can darken or fade under unsuitable conditions, affecting barcode readability. |
| Printer Compatibility | Provide printer model, media sensing method, print speed, and any ribbon requirements. | Compatibility depends on printer specifications, label dimensions, gap or mark sensing, and media construction. | Compatibility confirmation and a production trial using the buyer’s printer settings. | Testing helps identify feeding, sensing, adhesive, or print-quality issues before a large order. |
| Quality Control | Ask how the supplier controls dimensions, roll winding, splice frequency, print surface, and lot consistency. | Acceptance limits should be agreed in writing for the product and order; tolerances are supplier- and specification-dependent. | Inspection report, agreed specification, and batch or lot identification details. | Documented controls make incoming inspection and repeat orders more consistent. |
| Compliance and Documentation | Identify the destination market and the label’s intended contact or packaging use. | Regulatory requirements depend on the market and application. Do not assume one certificate covers every use or destination. | Applicable declarations, test reports, and material documentation relevant to the stated use. | Verifying documents against the actual application helps reduce customs and compliance risks. |
| Samples and Approval | Approve a sample roll before confirming mass production, including winding and packaging requirements. | Test actual label dimensions, barcode readability, adhesive performance, and roll fit on production equipment. | Signed sample approval or written confirmation of the approved specification. | Pre-production approval gives both parties a clear reference for manufacturing. |
| MOQ and Lead Time | Request the minimum order quantity, production lead time, sample lead time, and reorder schedule. | These terms vary with material availability, customization, order volume, and production capacity; obtain written estimates for each order. | Quotation listing quantities, lead times, validity period, and any setup charges. | Clear commercial terms support inventory planning and prevent assumptions about delivery dates. |
| Export and Shipping | Confirm packaging method, shipping marks, export documents, delivery terms, and destination port or address. | Shipping cost and transit time depend on shipment size, route, mode, and agreed delivery terms. | Pro forma invoice, packing details, and a shipment plan showing responsibilities and costs. | Clear logistics arrangements help buyers compare quotes on an equivalent basis. |
| Supplier Selection | Compare suppliers using the same specification, sample test, order quantity, and delivery destination. | Evaluate product fit, documented quality controls, communication, commercial terms, and repeat-order capability. | Comparable quotations, approved samples, specification documents, and references where available. | A consistent evaluation process is more useful than selecting a supplier on price alone. |